
RFID Tunnel & Conveyor Automation: High-Speed Verification Blueprint
The definitive industrial engineering manual for building 99.99% accurate conveyor RFID scanning tunnels. Master high-speed 1,200 tags/min singulation physics, optical photocell GPIO trigger state machines, and carbon-loaded RF absorber foam cavity null suppression for high-throughput warehouse logistics.

Conveyor Physics & Throughput
The Mathematics of Conveyor Dwell Time & Singulation Saturation
How line speed, packaging tag density, and reader packet overhead dictate read reliability.
When a corrugated shipping carton travels along a powered roller or belt conveyor at 1.5 m/s (300 ft/min),
the tag population inside the carton spends less than one second within the electromagnetic read zone. Achieving 100% inventory accuracy requires
balancing the physical exposure window against the mathematical limits of the EPC Gen2v2 Q-algorithm anti-collision cycle.
Where L_effective is the tunnel electrical length between the 3 dB beamwidth edges (typically 1.2 m to 1.8 m)
and v_belt is conveyor speed in meters per second. For a 1.5 m tunnel at 1.5 m/s, the dwell window is exactly 1,000 milliseconds.
Where R_sing is reader singulation throughput (750 to 1,100 tags/s) and N_tags is carton tag density.
To survive mechanical vibration and packaging shadowing, K_reads must be ≥ 3.0 (every tag singulated at least 3 separate times).
The 1,200 Tags/Minute Industrial Benchmark
In high-speed apparel distribution centers, sortation lines run at 2.0 m/s with cartons arriving every 1.5 seconds containing up to 30 items.
This represents an instantaneous throughput requirement of 1,200 items per minute. If the tunnel is shorter than 1.5 meters or
uses a legacy reader singulating below 800 tags/second, K_reads drops below 1.5, guaranteeing dropped tags and downstream false-reject alarms.
Interactive Simulation Engine
Conveyor Velocity & Multi-Tag Saturation Calculator
Model your warehouse conveyor line speed, carton item count, and tunnel length to verify your read redundancy multiplier.
Conveyor Dwell Time & Multi-Tag Saturation Simulator
Calculate your exposure window, anti-collision cycle limit, and minimum read redundancy (K_reads ≥ 3.0).
Target: ≥ 3.0x reads per tag for 99.99% accuracy
Engineering Assessment:
Each tag is inventoried ≥ 3.0 independent times across antenna polarizations. 99.99%+ read rate guaranteed in industrial production.
Hardware Control & Electrical Schematics
Opto-Isolated Photocell GPIO Wiring & Control State Machine
Why 24/7 continuous RF transmission ruins warehouse logistics, and how to wire an optical beam trigger to a fixed reader.
One of the most destructive beginner mistakes in RFID conveyor integration is leaving the fixed reader in continuous autonomous transmit mode. Running a 4-port reader at 30 dBm (1.0 W conducted power) 24 hours a day results in:
- Severe Stray Reads: Reading stationary tagged inventory on adjacent shelves, passing tote carts, or workers wearing RFID badges up to 10 meters away.
- Power Amplifier Thermal Throttling: Reader internal RF power amplifiers overheat, triggering automatic firmware power reductions that shrink read zones.
- Spectral Collisions: Continuous RF carriers blind neighboring handheld terminals and dock door portals operating in the same frequency band.
| State | Optical Sensor | Reader RF Output | Middleware & Sorting Action |
|---|---|---|---|
| 0. IDLE | Beam Unbroken | OFF (0 dBm) | Standby; zero RF leakage into warehouse. |
| 1. LEADING EDGE | Carton Breaks Beam | ON (30 dBm) | Firmware interrupt triggers LLRP ROSpec; starts inventory timer. |
| 2. INVENTORY | Inside Tunnel | Antennas 1..4 Cycling | Gen2v2 Q-algorithm singulates all EPC tags inside carton. |
| 3. TRAILING EDGE | Beam Cleared | Debounce Delay (+150ms) | Ensures trailing tags in long cartons are fully read. |
| 4. RECONCILIATION | Past Sensor | OFF (0 dBm) | OpenRFID validates scanned EPC list against ERP ASN manifest. |
| 5. ROUTE / DIVERT | Reaches Diverter | OFF | If match: pass to shipping. If discrepancy: fire GPIO Out 1 reject pusher. |
Electromagnetic Shielding & Physics
RF Absorber Foam, Waveguide Cutoff & Cavity Resonance Suppression
How bare metal enclosures create destructive multipath nulls, and how carbon-loaded pyramid foam eliminates signal bounce.
An unlined metal enclosure constructed from aluminum or stainless steel sheets acts as an electromagnetic cavity resonator.
Because conductive surfaces enforce the boundary condition that tangential electric fields must equal zero (E_tan = 0),
over 98% of RF energy reflects back into the enclosure.
The Destruction of Multipath Standing Waves
Reflected waves combine with direct line-of-sight waves. At points where reflected path lengths differ by an odd number of half-wavelengths:
Destructive vector cancellation causes deep spatial RF nulls (drops of -20 dB to -35 dB). Tags that pass through these null locations receive insufficient harvested power to energize their silicon charge pumps, resulting in random, unrepeatable misreads.
Waveguide Cutoff Physics at Tunnel Openings
A rectangular tunnel opening acts as an open waveguide. The cutoff frequency for the dominant TE_10 mode is governed by:
Because UHF RFID operates at 865–928 MHz (which is far above the 250 MHz cutoff), the opening cannot block RF waves naturally. Energy escapes directly into the warehouse without proper absorber vestibules and conductive flaps.
The 3-Step Shielding Engineering Standard:
Line the tunnel interior with 2-inch to 4-inch carbon-loaded polyurethane foam. The tapered geometry provides an impedance gradient matching free space (377 Ω) into lossy carbon, dissipating ≥ 20 dB of RF bounce.
Extend non-reading shielding vestibules at both ends. Vestibule length must satisfy L ≥ 1.5 × Aperture Height
to ensure escaping fringe fields undergo multiple bounces against absorber walls.
Never mount antennas pointing parallel to the openings. Angle sidewall antennas inward at 30° to 45° toward the center, directing the primary radiation lobe away from external conveyor lanes.
Laboratory & Field Testing
High-Speed Conveyor RFID Scanning Demonstration
Watch real-time multi-angle antenna cross-fire scanning cartons moving along an industrial automated sortation line.
Industrial RFID Conveyor Scanning Tunnel Demonstration
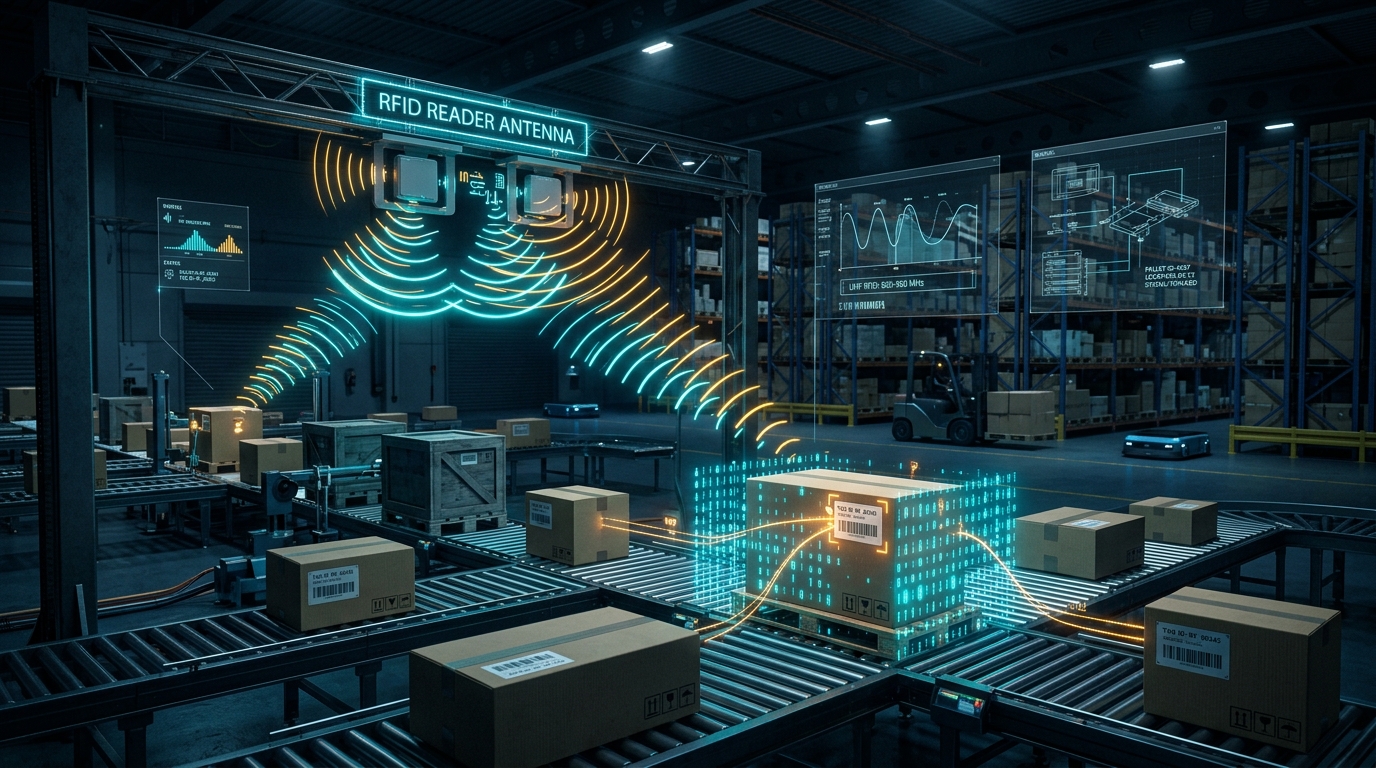
High-speed optical inspection and multi-antenna UHF RFID scanning of industrial cartons on a powered conveyor belt with GPIO photocell triggering.
Recommended Hardware Selection
Industrial Conveyor Tunnel Hardware Bill of Materials (BOM)
Enterprise-grade readers, antennas, inlays, and middleware engineered for 24/7 industrial logistics sortation.
Zebra FX9600 4-Port Fixed RFID Reader
Industry workhorse for conveyor tunnels. Features high RF sensitivity (-88 dBm), built-in opto-isolated 4-in / 4-out GPIO terminal, and rugged IP53 die-cast aluminum chassis. Supports POE+ and Linux on-reader embedded applications.
Impinj Speedway R700 Enterprise RAIN Reader
Built on the Impinj E710 chip core. Delivers industry-leading singulation speed exceeding 1,100 tags/second with -92 dBm receive sensitivity. Ideal for parcel hubs sorting at 500+ feet per minute with dense multi-item packages.
UHF Fixed Reader Circular Polarized Panel Antennas
9 dBi circularly polarized panel antennas with an axial ratio < 2.0 dB. Engineered for wide horizontal beamwidths inside compact conveyor enclosures, ensuring uniform field distribution across top, bottom, and side cross-fire planes.
NXP UCODE 9 Inlays & OpenRFID Edge Suite
NXP UCODE 9 delivers -24 dBm sensitivity and parallel converting capabilities. Combined with the open-source OpenRFID Edge Gateway, the system aggregates scanned EPCs into clean JSON streams and automatically reconciles against SAP, Tally, or custom WMS APIs.
Engineering FAQs
Frequently Asked Questions on RFID Conveyor Tunnels
Technical answers regarding conveyor line speeds, stray read prevention, GPIO integration, and absorber materials.
How do you calculate the minimum RFID tunnel length for a high-speed conveyor?
Minimum tunnel length is determined by belt velocity, tag population per carton, and reader singulation rate using the formula: L_min = (v_belt * N_tags * K_target) / R_sing. For a conveyor running at 1.5 m/s carrying 100 tags per carton with an enterprise reader singulating at 1,000 tags/s and a target read redundancy of K = 3.0, the minimum effective tunnel electrical length is: L_min = (1.5 * 100 * 3) / 1000 = 0.45 meters of core read aperture plus entrance/exit shielding vestibules of at least 0.9 meters, resulting in a total enclosure length of ~1.8 meters.
Why does unshielded metal inside an RFID tunnel cause tag read failures?
Bare aluminum or galvanized steel enclosure walls act as metallic cavity resonators. Because tangential electric fields must equal zero at conductive boundaries (E_tan = 0), incident RF waves reflect with over 98% efficiency. These reflections combine with direct line-of-sight waves to create standing waves with severe destructive interference nulls (depths of -20 dB to -35 dB) spaced every half-wavelength (~16.5 cm at 915 MHz). Tags located within these spatial nulls receive insufficient electromagnetic energy to charge their internal silicon rectifiers, causing 10% to 25% carton misread rates.
How does photocell GPIO triggering prevent false reads on adjacent conveyor lines?
Running RFID readers in 24/7 continuous autonomous inventory mode floods the warehouse with stray RF energy, inadvertently reading passing forklifts, neighboring conveyors, or staged pallets. Wiring a retro-reflective optical photocell to the reader's opto-isolated GPIO Input ensures the RF transmitter powers on only when a carton breaks the optical beam. Once the trailing edge clears and a 150 ms debounce delay elapses, the transmitter immediately cuts RF power to 0 dBm, ensuring 100% data isolation per carton.
What is the best antenna polarization configuration inside an RFID tunnel?
A 4-antenna cross-fire circular polarization configuration is the global benchmark. Two circular panel antennas are mounted on the left and right sidewalls canted 15 degrees inward, one top antenna faces straight down, and one bottom antenna radiates through a low-dielectric conveyor bed (e.g. UHMW polyethylene). Circular polarization guarantees electromagnetic coupling regardless of tag 3D angular rotation (X, Y, or Z axis) inside the packed carton.
What type of RF absorber foam is required for UHF RFID tunnels?
Tunnels require carbon-loaded polyurethane pyramidal foam with 2-inch to 4-inch pyramid heights (e.g., Eccosorb or C-RAM). The tapered pyramid geometry provides an impedance gradient that transitions the wave impedance smoothly from 377 ohms (free space air) into lossy resistive carbon matrices, attenuating reflected waves by 20 dB to 25 dB across global RAIN RFID frequencies (865–928 MHz).
Explore Related Technical Hardware & Engineering Guides
Deepen your RF engineering knowledge with our silicon benchmarks, antenna polarization guides, and link budget calculators.
RFID Silicon IC Directory →
Compare Impinj M800, NXP UCODE 9, and Alien Higgs silicon sensitivities and on-die AutoTune engines.
Circular vs Linear Polarization →
The physics of 3 dB polarization loss, axial ratio, and interactive 3D tag angle simulation.
RFID Read Range Calculator →
Calculate real-world line-of-sight range across EIRP, chip sensitivity, and environmental attenuation.